Minimizing Polishing: General Industry Coverage
END USER: Tech NH Inc., (603) 424-4404, www.technh.com. CHALLENGE: Reduce polishing time when producing hardened steel molds. SOLUTION: Long-reach, small-diameter endmills for hard milling. SOLUTION PROVIDERS: Harvey Tool Co. LLC, (800) 645-5609, www.harveytool.com; Industrial Tool Supply, (888) 200-8887, www.itslowell.com.
————-
END USER: Tech NH Inc., (603) 424-4404, www.technh.com. CHALLENGE: Reduce polishing time when producing hardened steel molds. SOLUTION: Long-reach, small-diameter endmills for hard milling. SOLUTION PROVIDERS: Harvey Tool Co. LLC, (800) 645-5609, www.harveytool.com; Industrial Tool Supply, (888) 200-8887, www.itslowell.com.
—————
Courtesy of Tech NH
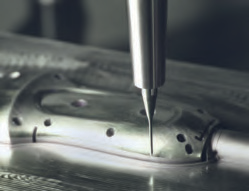
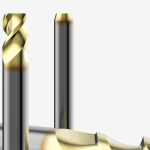
Tech NH applies small-diameter, long-reach endmills from Harvey Tool, such as this 0.047 “-dia., 2-flute, AlTiN-coated one, to hard mill many mold features that were previously EDMed.
Tech NH Inc., Merrimack, N.H., provides molding services including engineering and manufacturing molds and injection molding parts. The shop performs prototype and custom work, as well as production runs from a few thousand to several million pieces.
The molds Tech NH produces often are complex and require fine surface finishes. Achieving those finishes typically required up to 50 hours of polishing time after EDMing. To mill graphite EDM electrodes, Wayne Burgett, toolroom manager, had been applying PVD-amorphous-diamond-coated miniature endmills from Harvey Tool Co. LLC, Rowley, Mass. Seeking to maximize tool life in the abrasive material, Burgett wondered whether Harvey Tool could coat the tools with CVD diamond, estimating that the thicker coating could extend tool life eight to 10 times.
Tim Stimson, sales representative for distributor Industrial Tool Supply, Lowell, Mass., brought Harvey Tool representatives to Tech NH.
In addition to confirming the availability of CVD-coated tools for machining graphite, the Harvey Tool personnel “wanted to look at my other processes,” Burgett said. “They just happened to come in when we were producing a twin- cavity mold made of 48- to 53-HRC 420 stainless. The required finish was almost a mirror.”
Harvey Tool was able to provide small-diameter, long-reach endmills that enabled Tech NH to hard mill many mold features that were previously EDMed. Hard milling imparted a finer surface finish than EDMing, enabling Tech NH to achieve the mirror-like finish with only 5 to 6 hours of polishing instead of the 40 to 50 hours necessary when EDMing was more extensive. (Tech NH still EDMs some small features that a milling tool can’t access.) In addition, Burgett said, “We are saving time on electrode design, graphite milling, EDMing and programming.”
View print ads from this spread
Review the ads on this magazine spread to continue reading. Each ad takes two seconds; a two-page ad counts once.
Advertisers on this magazine spread
Print placements on this magazine spread
Tungaloyamerica
www.tungaloyamerica.com
3726 N. Ventura Dr. Arlington Heights, IL 60004 scan for instant IS #43.
www.tungaloyamerica.com 3726 N. Ventura Dr. Arlington Heights, IL 60004 scan for instant IS #43 ph: 888-554-8394 fax: 888 -554-8392 web access
Visit Tungaloyamerica View this placement in the issue recordPrint ads from this magazine
3726 N. Ventura Dr. Arlington Heights, IL 60004 scan for instant IS #43.
www.tungaloyamerica.com 3726 N. Ventura Dr. Arlington Heights, IL 60004 scan for instant IS #43 ph: 888-554-8394 fax: 888 -554-8392 web access
Continue reading
July 2011
To mill complex mold contours, Tech NH uses small-diameter cutters with stub-length flutes. “I don’t need long flutes, I just need reach,” Burgett said, “because everything we are doing is 3-D and has draft angles. Plus, the stubby cutters are more rigid. On the ⅛”-dia. tool, I might go up to a 1⅞” or 2″ length, and I use quite a few 0.010″-dia. ball mills with a ⅛” reach.”
According to Burgett, a major advantage of using Harvey tools is immediate availability of what otherwise would be specials requiring long lead times. Marcus Ralston, Harvey Tool vice president of sales and business development, said, “Shops ordinarily have to order these tools as specials, pay an additional cost for lower quantities and wait a long time. We take that same product and make it a standard-stock inventoried item, and we can have it to the shop the next day.”
According to Ralston, the endmills for hard milling from Harvey Tool feature proprietary geometries and an advanced AlTiN coating.
Depending on the complexity of the part, Tech NH can move from an initial quote for a job to a finished mold in 4 to 8 weeks, Burgett noted. In addition to quick delivery of “standard special” tools from Harvey Tool, he credits the rapid turnaround to “all the other new technology. Last year we got a new F3 vertical machining center from Makino.” Most important, he said, is the skill and commitment of Tech NH employees.
Glossary terms in this article
Related
Subscribers can use MFGAxis notes, saves and discussion tools with their innoNET account.