No monkeying around: Drilling Performance
END USER: D&G Precision Manufacturing Inc., (920) 477-3609, www.dgmfg.com. CHALLENGE: Decrease cycle times when milling aluminum forgings. SOLUTION: Two-flute solid-carbide endmills.
View print ads from this spread
Review the ads on this magazine spread to continue reading. Each ad takes two seconds; a two-page ad counts once.
Advertisers on this magazine spread
Print placements on this magazine spread
Dgmfg
productive times
No monkeying around D&G Precision Manufacturing Inc., from repairing a single part to produc- Eden, Wis., is a family-owned and -op- ing prototypes to machining a full pro- END USER: D&G Precision erated job shop started in 1994 by the duction run. Manufacturing Inc. CHALLENGE: Decrease cycle times when milling aluminum forgings
productive times No monkeying around D&G Precision Manufacturing Inc., from repairing a single part to produc- Eden, Wis., is a family-owned and -op- ing prototypes to machining a full pro- END USER: D&G Precision erated job shop started in 1994 by the duction run. Manufacturing Inc. father-and-son team of Gene, CEO, and One recent job came from a company (920) 477-3609 David Dallapiazza, president. Jobs range that “basically had too much work to do www.dgmfg.com CHALLENGE: Decrease cycle times when milling aluminum forgings.
Visit Dgmfg View this placement in the issue recordPrint ads from this magazine
No monkeying around D&G Precision Manufacturing Inc., from repairing a single part to produc- Eden, Wis., is a family-owned and -op- ing prototypes to machining a full pro- END USER: D&G Precision erated job shop started in 1994 by the duction run. Manufacturing Inc. CHALLENGE: Decrease cycle times when milling aluminum forgings
productive times No monkeying around D&G Precision Manufacturing Inc., from repairing a single part to produc- Eden, Wis., is a family-owned and -op- ing prototypes to machining a full pro- END USER: D&G Precision erated job shop started in 1994 by the duction run. Manufacturing Inc. father-and-son team of Gene, CEO, and One recent job came from a company (920) 477-3609 David Dallapiazza, president. Jobs range that “basically had too much work to do www.dgmfg.com CHALLENGE: Decrease cycle times when milling aluminum forgings.
Continue reading
March 2010
————–
END USER: D&G Precision Manufacturing Inc., (920) 477-3609, www.dgmfg.com. CHALLENGE: Decrease cycle times when milling aluminum forgings. SOLUTION: Two-flute solid-carbide endmills. SOLUTION PROVIDER: Gorilla Tools, (866) 888-9600, www.gorillamill.net
————–
Courtesy of Gorilla Tools
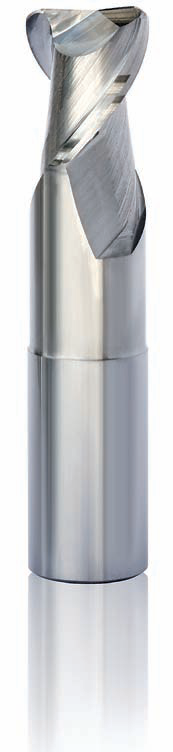
An uncoated 2-flute endmill from Gorilla Tools enabled D&G Precision Manufacturing to significantly increase the feed rate and tool life compared to a previously applied uncoated 3-flute tool.
D&G Precision Manufacturing Inc., Eden, Wis., is a family-owned and -operated job shop started in 1994 by the father-and-son team of Gene, CEO, and David Dallapiazza, president. Jobs range from repairing a single part to producing prototypes to machining a full production run.
One recent job came from a company that “basically had too much work to do and they offloaded it on us, which we were more than happy to help them out with,” said Henry T. Potocki Jr., D&G’s process engineer.
The job required milling, drilling and chamfering aluminum forgings to produce risers. In addition to supplying the 9-lb. workpieces, which require removing about 78 percent of the material, the customer supplied the first round of cutting tools, toolholders and other tooling. “The whole nine yards, everything they were using,” Potocki said. “They were really hot to get the parts.”
The customer, however, was running its machine 24/7 and using a pallet changer to load and unload parts, whereas D&G doesn’t have the ability to machine parts around the clock and has to manually load and unload parts into one of its 40-taper Mori Seiki Dura vertical 5100 mills. “I needed to decrease my cycle time considerably to make up for that,” Potocki said.
Over the years, D&G has developed a relationship with Gorilla Tools in nearby Waukesha, Wis., and initially replaced the drills in the customer’s tooling package with ones from Gorilla.
Next, Potocki discussed the milling operations with Mark Greenwood, national sales manager for Gorilla Tools, to determine how D&G could reduce cycle times for the 3-flute endmills it was running. “He said, ‘we’ve got a new 2-fluter that we’re in the process of fine-tuning. How do you feel about running it? It should handle the chip evacuation and decrease cycle times,’ ” Potocki said, noting that the uncoated 2-flute tool has a larger flute space than the uncoated 3-flute tool. “Obviously, I’m in business to make parts faster.”
Lloyd Cribb, D&G’s programmer, reprogrammed the milling operations to take full advantage of the new tools, and the company ordered two sets of four diameters: 1⁄8 “, 7⁄16 “, ½ ” and ¾ “. Compared to the 3-flute endmills, D&G was able to significantly increase the feed rate. The feed went from 45 to 80 ipm for the 1⁄8 ” tool, 45 to 120 ipm for the 7⁄16 ” and ½ ” endmills and 80 to 100 ipm for the ¾ ” tool.
D&G runs all the endmills at the machine’s maximum spindle speed of 10,000 rpm. “We don’t have enough spindle speed to drive the tools as fast as we could,” Potocki said, adding that if the project becomes a long-term job the shop may acquire spindle speeders to achieve 30,000 rpm for the smaller tools. “When you hear the tools run, you just know they can take a lot more than what we’re doing.”
In addition to running faster, tool life increased more than six times compared to the previous tools. After producing about 6,500 parts, D&G changed its first set of tools. In contrast, D&G changed the original tools after producing about 1,000 pieces. At the Wisconsin Machine Tool Show in October, Potocki met Greenwood, who asked how the project was going. “Because we hadn’t ordered any additional tools at that time, his concern was that the project failed,” he said.
When the Gorilla Tools are worn, D&G sends them to the toolmaker for regrinding. “I’m a fan of that, knowing that they made the tool and should know how to regrind the tool,” Potocki said.
He noted that the shop predominantly applies Gorilla Tools for its milling operations, estimating that the tools reduce cycle times by 50 percent compared to other tools.
Glossary terms in this article
Related
Subscribers can use MFGAxis notes, saves and discussion tools with their innoNET account.