Modular Workholding: Beyond the Hype
A practical guide to deciding when quick-change fixtures earn their place on the shop floor.
A practical guide to deciding when quick-change fixtures earn their place on the shop floor.
Read the trade journals, visit the trade shows and talk to the local sales rep, and they will all say the same thing: You can’t continue in the machining business without their super-advanced workholding technology.
Workholding is the most critical factor in machining. Advanced cutting tools, the best machine tools and the best CAM software are useless if you cannot hold the workpiece. “How am I going to hold it?” is the first question each machinist or toolmaker asks.
Modern machinists have countless workholding options. In recent years, the chipmaking industry has made a concerted effort to promote and adopt modular workholding devices designed to reduce setup times and costs. Investing in these devices can be very expensive, but it also can have a significant impact on cost and profit.
It is easy to succumb to the pressures of a good marketing campaign or be lured into a purchase after seeing a convincing demonstration at a trade show. I know—it has happened to me more than once. So how does a shop justify new workholding, and what factors should it consider before purchasing?
The first consideration is volume. I’m not talking about automotive volumes, where each machine is dedicated to a specific part or feature. That kind of work always will demand dedicated fixtures and complex automation. I am talking about small manufacturers or job shops that do not have dedicated machine tools and run varying quantities for their customers.
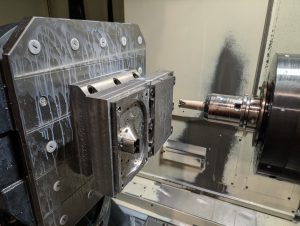
Modular workholding can be advantageous when quantities are low. While it sounds counterintuitive, shops that make one or two parts at a time can benefit from modularity. Let’s say your shop makes a specialized product to order, and each order requires a small number of machined parts. A VMC or HMC can be outfitted with a modular base, with each component mounted on the movable workholding component. Simply load the parts onto the base, select the proper program, and making one or two parts becomes easy and cost-effective.
By combining CAD, CAM and modular fixtures, a shop can reduce changeover time to a few minutes. Modular workholding provides the foundation. Each dedicated fixture is built virtually in the CAD system for accuracy. The part and workpiece models are transferred to the CAM system, where programs are created with a common origin. Once the modular workholding base is located on the machine and its origin is set, every program and movable workpiece fixture is oriented and ready for use. This eliminates the need to align fixtures and set work coordinates. With multiple modular bases positioned on the machine, it is possible to locate large and small workpieces without altering the machine.
Likewise, it is possible to place the base component on an HMC tombstone and load a wide variety of parts onto the base fixtures. With probing, chip readers and similar technology, the HMC can recognize which workpiece has been loaded, automatically select the correct program and execute the machining cycle. In these cases, modularity allows profitable machining of low-volume parts.
Tight tolerances dictate better workholding. As every machinist knows, accuracy is negatively affected each time a part is removed from the workholding device and repositioned. Modular workholding systems help reduce this impact. When a workpiece must be repositioned for access, a modular fixture might be the right choice. Modular workholding devices are extremely repeatable, often measured in a few tenths (0.0001 inch). A part with tight tolerances can be securely attached to the movable portion and moved across bases held in different orientations, reducing errors caused by removing the workpiece from the fixture.
Each new part requires the shop to make a new fixture that can be held by the modular base, which is more costly than using traditional workholding devices such as chucks and vises. However, when workpieces are nonprismatic or flimsy, a modular fixture allows the shop to efficiently manufacture a dedicated fixture that compensates for irregularities while reaping the quick-change benefits of modular workholding.
When a traditional vise or chuck is the best choice, it can be outfitted with modular hardware and used on the modular base. The accuracy of the modular base allows the machinist to install chucks and vises without performing alignment, saving setup time and reducing workholding costs. Modular workholding coupled with vises and chucks is a great way to begin using modular workholding. The reduced setup times and improved accuracy can be assigned a value and then used to convince the guardian of the purse to invest in more modular devices.
Most importantly, modular workholding, paired with other technologies, is a force multiplier in the machine shop. We know skilled machinists are hard to find. With modular workholding and the resulting reductions in setup time and errors, a good machinist can create a repeatable process that less-skilled operators can replicate. This frees the skilled person from monitoring a machine and allows their skills to be spread across the shop.
Which brand is best? The one you are most comfortable with. All modular workholding products from respected manufacturers share similar technology and geometry, tweaked to avoid infringement. All of them are good, and their accuracy is essentially the same. Choose the brand that offers the best service and sales support in your area. It is also a good idea to consider longevity. Does the manufacturer have a proven record of producing high-quality, accurate workholding? Does its modular product have a proven record of success? If the company has been building the product for several years and can demonstrate repeated successful applications, it is probably a safe choice.
If I were starting a new shop, I would invest heavily in modular workholding to take advantage of the benefits named above. The ability to open the door, put the workpiece in place and initiate the machining process with minimal input is the foundation for successful machining operations in today’s market. Conditions in today’s chipmaking industry dictate that you can’t afford to ignore modular workholding.
Related
Subscribers can use MFGAxis notes, saves and discussion tools with their innoNET account.