No Hands Required for Deburring
Parts manufacturers achieve a variety of advantages when performing CNC deburring in a machining center or robotic setup instead of manually. The gains include deburring with a high level of efficiency and repeatability and extended tool life. Deburring by hand is also a tedious operation that workers do not look forward to performing.
Parts manufacturers achieve a variety of advantages when performing CNC deburring in a machining center or robotic setup instead of manually. The gains include deburring with a high level of efficiency and repeatability and extended tool life. Deburring by hand is also a tedious operation that workers do not look forward to performing.
“The more you can get done in your equipment rather than by hand is definitely where everyone is heading,” said Steve Alviti Jr., vice president of Bel Air Finishing Supply Corp. in North Kingstown, Rhode Island.
Nonetheless, there are still plenty of people deburring manually, he added. “We see a lot of that every day.”
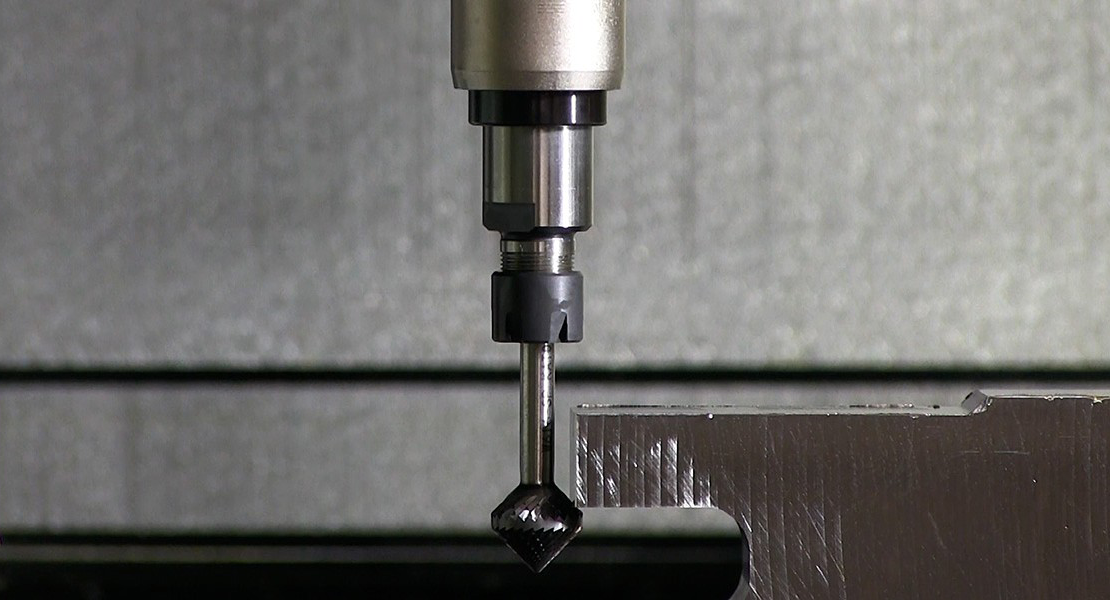
For medium to “gross” deburring, Bel Air Finishing supplies the FM-DBR7-1D and FM-DBR7-SC-ADJ series CNC deburring toolholders from Kato Machinery Co. Ltd. in Japan. According to the company, the former, or 1D, series is suitable for automated front- and back-side edge finishing of machined features, such as holes, in a single pass while the latter series is for front-side deburring and chamfering in CNC machining centers and automated systems.
“You’re saving a lot of time after your machining process by doing that deburring in the CNC machine,” Alviti said.
Compared to using the holders in a vertical or horizontal machining center, he noted that about 10 to 15 percent of end users debur with the tools in a robotic system. “I would tailor it to whatever the client’s solution is.”
The 1D series provides 10 mm (0.39″) of floating tension and compression to compensate for dimensional tolerances and prevent chatter, Alviti explained, and the fully adjustable spring-load SC-ADJ series provides 10 mm (0.39″) of floating compression. “You’re able to simplify your process into one step with one tool.”
Floating CNC deburring toolholders use a spring-loaded or telescopic mechanism that allows the cutting tool to move axially while maintaining consistent contact with the part. The 1D series features three spring-load options for controlled pressure: yellow (soft), green (medium) and red (hard). Using the yellow option leaves a smaller landing on the targeted edge than the other two, while the red one leaves the largest, or thickest, landing on the part edge.
Alviti added that if an end user is deburring different types of edges on one component or deburring different types of parts, adjustments can be made on the toolholder without removing it. “The harder that you have that spring tension, the more aggressive deburring you’re getting, plus the larger chamfer that you leave behind.”
Another way to adjust the spring-loaded capabilities of those holders is by changing the machining parameters, Alviti said. “If you want the chamfer to become smaller on each step, you would increase the feed and speed. If you want the chamfer to become larger, you would reduce the feed and speed.”
Bel Air Finishing will not perform deburring trials in a CNC machine, but the company will conduct evaluations to determine if the deburring toolholders are an appropriate solution, he said. The majority of the time a toolholder is suitable, but it can be overkill when a shop already has a post process in place that can perform the needed deburring. “You don’t want to add an extra step in your machining op when you don’t have to.”
When the application is appropriate, such as deburring a high volume of cast automotive parts like housings and hydraulic pumps, Alviti said a CNC deburring toolholder is an effective tool for the job. “We haven’t seen a burr that’s been bad enough to beat it.”
Prepare to Float
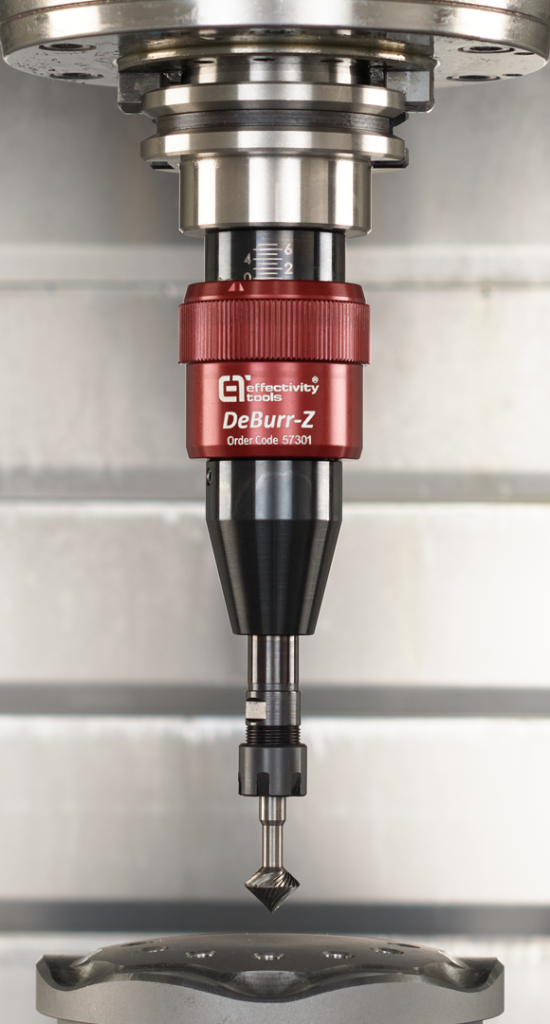
Tapmatic Corp. is another provider of toolholders for CNC deburring. The company offers the DeBurr-Z holder with straight shank and ER collet that floats in both the compression and extension direction, allowing the deburring tool to follow the top edges or underside edges of the workpiece even when these edges are not clearly defined, Tapmatic reports.
Floating in the compression direction, said Mark Johnson, president of the Post Falls, Idaho, toolmaker, allows the burr cutting tool to follow and deburr the top edge of the workpiece. “You don’t have to program it exactly to follow the edge because the holder has 10 mm of compression float, maintaining that contact as long as it’s within that 10 mm range.”
Conversely, the tension float, which is also up to 10 mm, allows deburring of the underside edge, he added. A common application is deburring castings, such as cast iron, steel and aluminum ones for the automotive and aerospace industries.
When deburring a workpiece with a high level of hardness or when a large edge break is required, Johnson explained that an end user can adjust the preload of both the compression spring and the extension spring without replacing springs or taking anything apart. “It’s all adjusted through a collar, or sleeve, on the body of the DeBurr-Z. You don’t have to remove it from the machine or from the shank.”
With a deburring tool in position, the spindle speed is typically from 5,000 rpm to a maximum of 10,000 rpm, and the feed rate is anywhere from about 30 to 80 ipm, depending on the workpiece material and the desired edge break, he said.
Review the print ads from this magazine to continue
This quick advertiser review unlocks the rest of the article and keeps the full-screen reader focused on the ads instead of the page chrome.
Advertisers included in this article experience
Print placements connected to this article
J.W. Done
ORBITOOL Deburring Tools
J.W. Done promotes ORBITOOL deburring tools for cross-hole deburring.
ORBITOOL deburring tools are promoted for deburring cross holes, with a guaranteed or money-back message.
Visit J.W. Done View this placement in the issue recordEltool
Integrate Secondary Operations
Eltool promotes Titespot angle heads for turning bores, oil grooving, keyway cutting and secondary operations.
Titespot angle heads can integrate oil grooving, keyway cutting and other secondary operations into turning operations.
Visit Eltool View this placement in the issue recordPrint ads from this magazine
J.W. Done promotes ORBITOOL deburring tools for cross-hole deburring.
ORBITOOL deburring tools are promoted for deburring cross holes, with a guaranteed or money-back message.
Continue reading
May 2026
In addition to being used in a CNC machine, Johnson noted that DeBurr-Z is suitable for use in a robotic system. Typically, coolant is not needed. “Any application where you need some axial compensation, you could use it.”
Depending on the application, Tapmatic also offers spherical and angular carbide burs for use in the holder. The offerings include angular tools for 60° and 90° top edge deburring and 28° underside edge deburring, as well as spherical cutters. “The spherical tool is helpful is you’re wanting to do both top and underside edges,” he said.
DeBurr-Z is also used for engraving, he said, and Tapmatic offers tools that can both engrave and perform 90° top and underside edge deburring. “The benefit of having that compression float for engraving is that you can approach the workpiece more quickly, and it can give you better life of the engraving tool.”
Down to Size
Part of Heule Tool Corp.’s line of deburring/chamfering tools targets the removal of burrs from small-diameter bores. “Heule’s been concentrating on automation and deburring for over 60 years now, and it’s always been getting smaller and smaller products to address a lot of different industries,” said Gary Brown, president – North America for the Loveland, Ohio, toolmaker.
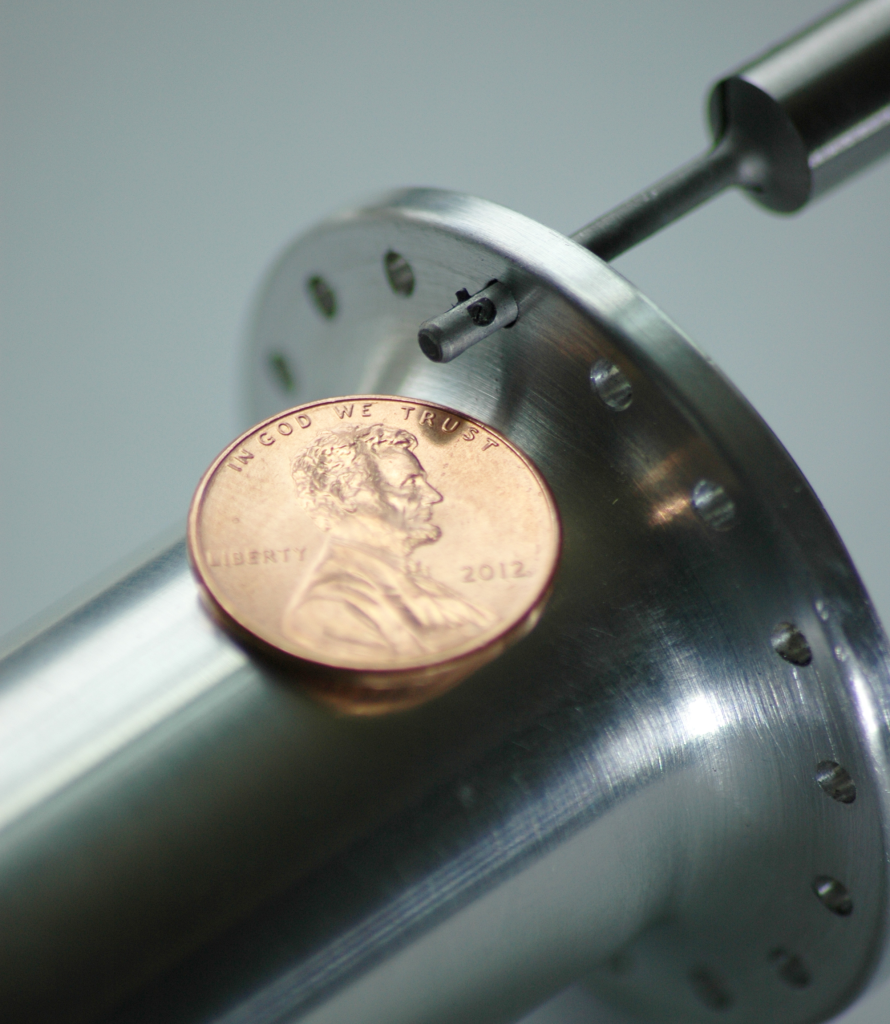
After getting down to 2 mm (0.079″), Heule Tool introduced the DL2 line for bore diameters from 1 to 2.1 mm (0.039″ to 0.083″). “It’s very difficult to hand bench these holes,” he noted. “You need a reliable tool to automate and avoid that manual intervention and get it done on the CNC machine.”
Brown added that customers have successfully used the product in robotic applications. Also, the DL2 tool is suitable for manual operation, such as for deburring a minimal number of holes produced on a drill press, but it is designed for higher production, automated applications. “We don’t discourage it, but we would recommend always to have controlled feeds and speeds, so you get consistency on a CNC machine rather than trying to hand bench and guessing some feeds and speeds. It’s just accuracy.”
There are 14 variations of DL2 tool, with each one targeted to deburr the exact hole size and enhance the accuracy of the operation, Brown explained.
The DL2 has a four-part construction where the blade is integrated into the spring to form a single unit, the company reports. This design enables quick blade replacement without tweezers or magnifying tools.
He explained that the tool features through-coolant capability, directing fluid precisely to the cutting edge of the carbide blade to ensure effective chip removal, consistent performance and process safety. “It just allows a cleaner deburring situation. Because the holes are small, you get more lubrication, so you don’t get any material build up.”
Brown said the carbide inserts for the tool are available with two types of coatings: AlTiN and a diamond-like coating (DLC) for nonferrous materials. In addition to other benefits, a coating also helps minimize BUE. “If you look out at the industry, there are very few uncoated carbide inserts anymore.”
The DL2 is suitable for deburring flat and curved surfaces up to about 6° to 10°, he noted. “It’s not quite as forgiving as our COFA product line, which can handle up to 20°.”
The cutter geometry is positive to help deburr difficult-to-deburr workpieces, such as nickel-base superalloys that tend to workharden, Brown said. “We do a unique thing where we run left-hand cutting inserts. Our tools and cutting blades cut counterclockwise, or left-hand cutting, opposite of the drill rotation and burr formation. It makes it easier for deburring more aggressively because your drill is pushing the burr to the right and we’re taking the burr off to the left.”
While the DL2 is ideal for watchmaking applications and deburring critical devices such as surgical instruments, Brown said the tool is frequently used for deburring other types of holes, such as vent holes in smartphones and oil cross-holes. “Our largest customer is actually an automotive shock producer.”
contributors
Bel Air Finishing Supply Corp.
401-667-7902
belairfinishing.com
Heule Tool Corp.
513-848-7235
www.heuletool.com
Tapmatic Corp.
800-854-6019
www.tapmatic.com
Related

 MFGAxis Discussion
Be part of the shop-floor conversation
Like, save, or comment on this CTE story.


MFGAxis Discussion