Workholding Elevates Training Capability
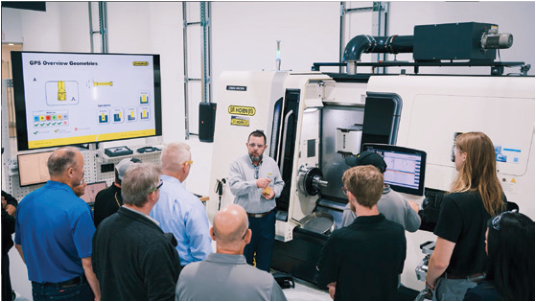
As an international manufacturer of high-precision tooling, HORN USA in Franklin, Tennessee, understands the need for proper training to ensure that distributors and customers achieve the maximum benefit from its products. That commitment is demonstrated by the HORN Academy Demo Center, which opened in January 2025 at the company’s headquarters.
As an international manufacturer of high-precision tooling, HORN USA in Franklin, Tennessee, understands the need for proper training to ensure that distributors and customers achieve the maximum benefit from its products. That commitment is demonstrated by the HORN Academy Demo Center, which opened in January 2025 at the company’s headquarters.
- END USER
- HORN USA Inc.
615-771-4100
www.horn-group.com - SOLUTION PROVIDER
- HAINBUCH America Corp.
414-358-9550
www.hainbuchamerica.com - CHALLENGE
- Ensure that distributors and customers maximize the benefits of the toolmaker’s cutting tools at its training center.
- SOLUTION
- A quick-change workholding system.
The Demo Center is equipped with several machine tools and typically hosts eight standard training sessions for distributors and end users each year, along with two or three customer-specific sessions and five or six end-user projects.
Because HORN manufactures special broaching holders for customers that need tools developed within short timeframes, customized sessions can be arranged. The Academy also produces videos that allow customers to explore HORN products on their own schedules.
Academy Manager Edwin Tonne explained: “I started in the carbide cutting tool business in 1994, and I would say that what differentiates HORN in the market is our speed, commitment to precision and consistency in production. We manufacture around 27,000 standard items, and both they and our made-to-order products are produced to micron tolerances. The goal of our quality system and corporate culture is the elimination of variability in the finished product, and the Demo Center is dedicated to helping our end users achieve that end.”
Training sessions provide an in-depth overview of product lines and applications, including proper setup, carbide grades, cutting conditions and practices to maximize productivity and tool life. Standard sessions typically run for two days and cover two main topics during the week. Most parts range from 12 mm to 100 mm (0.472″ to 3.94″) in diameter.
“Around 90% of what we demo are standards, so we can always find something useful to show,” Tonne said. “On custom parts, we can assist customers by making trial cuts to ensure that their tools will work as expected.”
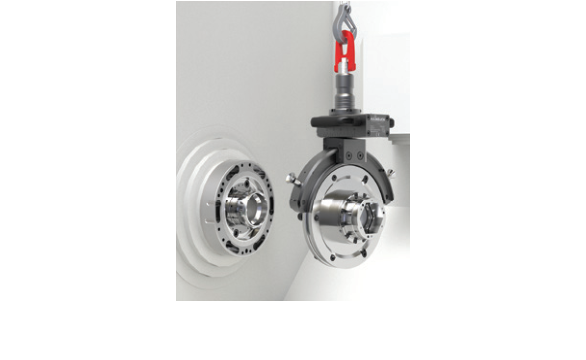
The HAINBUCH centroteX precision workholding system is key to tool performance at the center. Michael Larson, marketing director at HAINBUCH America Corp. in Germantown, Wisconsin, said, “At its core, centroteX is a high-precision, quick-change workholding system for CNC turning centers. Instead of spending 30 to 60 minutes removing a chuck, installing another one, indicating it and making adjustments, operators can complete a workholding changeover in less than two minutes.
“The real value isn’t just the speed. It’s the repeatability. CentroteX can provide interface repeatability of 3 µm (0.00012”) or less, allowing users to swap workholding devices and get right back to making parts without indicating or readjusting the setup. Another key benefit is rigidity. The interface is extremely solid, which helps improve consistency, accuracy, process stability and tool life.”
View print ads from this spread
Review the ads on this magazine spread to continue reading. Each ad takes two seconds; a two-page ad counts once.
Advertisers on this magazine spread
Print placements on this magazine spread
HAINBUCH America
HAINBUCH America — October 2026
Printed 27 in the October 2026 issue of Cutting Tool Engineering.
Visit HAINBUCH America View this placement in the issue recordPrint ads from this magazine
Printed 27 in the October 2026 issue of Cutting Tool Engineering.
Continue reading
October 2026 | Vol. 78 | Issue 8
Tonne concurred: “For us, repeatability is the most critical element of the system. For our S117 broaching holders, we need micron-level accuracy. The clamping elements we use need to be absolutely perfect to hold that tolerance. We also require the quick-change capability. During training, it is especially important to be efficient with time while maintaining a high level of safety. We don’t typically change out a chuck in the middle of a demo, but if we need to, we can change the entire chuck quickly and continue with the training exercise.”
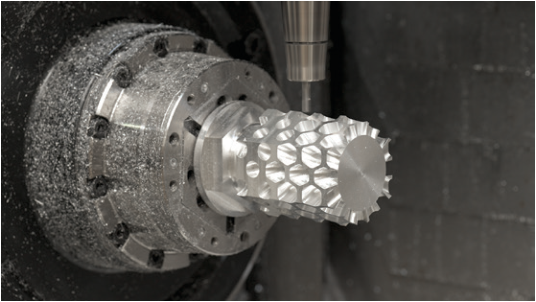
The centroteX system at HORN USA uses a TOPlus hexagonal chuck developed by HAINBUCH to increase holding power and resist contamination. “One of the best features of the TOPlus is ease of use,” Tonne said. “We can change material diameters in less than a minute without sacrificing precision. The component runout is perfect every time. This removes uncertainty from the process, which is great when you have 16 machinists standing in front of the machine. We know that the part is not going to move, and we can reduce our clearance planes because we know it is not going to run out. This also allows us to push our tools harder because we know the clamping force will be high and the part is not going to slip.”
A significant advantage of the centroteX system is the availability of additional components, including clamping heads in different sizes, said Josh Rainey, regional sales manager for HAINBUCH. “We make it a policy to maintain close contact with our customers. Typically, centroteX users are involved in a wide spectrum of parts and operations. We have an extensive variety of clamping heads in multiple size ranges and, where necessary, our engineering department can work with customers to design specialized components.”
Tonne added that HORN has purchased several serrated and smooth clamping heads since the machine was installed. “If we need another size, we can get it on site in a few days. We also have a few custom-designed collets, and they were delivered on schedule.”
Ultimately, the centroteX system’s quick-change capability and versatility result in significant time and cost savings, Tonne said. “We emphasize the importance of using quality workholding as part of the entire system. Our customers are very discerning, so they expect we will be using the best equipment available, both in terms of machinery and workholding. An especially favorable aspect of the centroteX system is the fact that the changeover procedure is very straightforward, fast and safe. Other systems I have used relied on brute strength to change out chucks, and there was always a risk of misalignment.
“For me, the principal challenge in instructing distributors and end users is keeping distractions and errors to a minimum. When we don’t spend the necessary time changing out workholding, there is more time to answer questions or go into greater detail on a specific topic. The training is far better when we move at a fast enough pace to cover everything they expect and more.”
Related
Subscribers can use MFGAxis notes, saves and discussion tools with their innoNET account.