Skip to content
Magazine Column

Feature Article

Select one or more.
Select one or more.
Select one or more.
Select one or more.
Reset

Latest in Feature Article

Smoother Roughing
Article May 1, 2000 Kip Hanson
Smoother Roughing
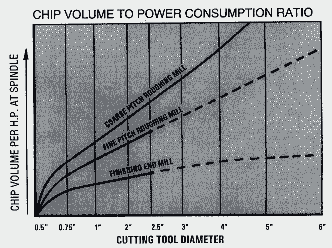
The author discusses the disadvantages of using a finishing endmill for roughing applications. He also presents a quick, systematic, step-by-step series of calculations that allows machinists to optimize metalcutting when applying coarse-pitch, cobalt-HSS roughing endmills.
Abrasive Personality: Drilling Performance
Article May 1, 2000 Kimberly R. Pontius
Abrasive Personality: Drilling Performance
High-silicon aluminum--aluminum that consists of at least 11.8 percent silicon--has qualities such as lightness and strength that appeal to automakers. The abrasives nature of the material, however, makes it difficult to machine. The author offers suggestions for milling, tapping, drilling, turning and grinding high-silicon aluminum.
Getting to the Bottom of Chatter
Article April 1, 2000
Getting to the Bottom of Chatter
Tool chatter is one of the biggest obstacles to effective machining that job nshops face. The author discusses the sources of chatter and offers nsuggestions for minimizing it.
Added Dimensions: 5-Axis Machining
Article April 1, 2000 Dennis Esford
Added Dimensions: 5-Axis Machining
A rotary table allows a 3-axis vertical machining center to machine in the n4th and 5th axes. The author explains the different types of rotary tables nthat are available and discusses the advantages and disadvantages of each.
High Expectations: Drilling Performance
Article April 1, 2000 Mark Richardson
High Expectations: Drilling Performance
People in the aerospace industry expect a lot from reamers. The author, an nengineer who works for a manufacturer of aerospace components, discusses nstrategies for job shops interested in developing a precision reaming nprogram.
Don’t Toss that Indexable Tool
Article April 1, 2000 Derek Phillips
Don’t Toss that Indexable Tool
Ninety-nine percent of indexable tools that break can be repaired, according to companies that repair tools. And, they say, a broken indexable tool can nbe repaired so it performs as well as or better than the original.
Company Saves Big with Custom Indexable Tool
Article April 1, 2000 Derek Phillips
Company Saves Big with Custom Indexable Tool
Switching from a brazed-tip trepanning tool to an indexable-insert tool nreduced downtime for a manufacturer of cast iron cylinder heads by 45 nminutes. And, incredibly, the price-per-piece dropped so much that the ncompany could save $690,000 annually.
Getting a Better Edge: Design & Engineering
Article March 1, 2000 William Shaffer
Getting a Better Edge: Design & Engineering
The author, an expert on cutting tool edge preparation, explains the importance of applying the proper edge hone to a tool. He also discusses a brush-type honing machine designed to apply a variable edge--a capability not available with other machines on the market.
Creeping Up
Article March 1, 2000 Dennis Esford
Creeping Up
Creep-feed grinding is not as popular a process as it was predicted to become in the late 1980s. But a machine shop that specializes in CF grinding has found great success by using the process. The shop's owner and other CF-grinding experts contend that as workpiece tolerances become tighter and manufacturers begin using more exotic workpiece materials, CF grinding will grow in popularity.
Software Solutions: Safety, Standards & Compliance
Article March 1, 2000 Dennis Esford
Software Solutions: Safety, Standards & Compliance
Tool management software is designed to help users of cutting tools get more control of their toolcribs. The article describes the types of tool management software available, the savings possible by utilizing software and includes comments from shop owners who've installed these systems.

Keep exploring