Skip to content
Operation / Process

Machining

Optional: narrow results to one content type.
Select one or more.
Select one or more.
Select one or more.
Reset

Latest in Machining

Selecting Coolants: Why and How
Article October 1, 1995 William Sluhan
Selecting Coolants: Why and How
This is the first in a series of Articles on coolants. It provides a general review of the types of fluids available, their cooling and lubricating abilities and their ease of disposal. Criteria are offered for selecting the appropriate fluid for an operation.
Beyond the Ban: General Industry Coverage
Article October 1, 1995 Norm Semple
Beyond the Ban: General Industry Coverage
The EPA's ban on ozone-depleting chemicals had an impact on the formulation of metalworking fluids containing 1,1,1 trichloroethane. This article looks at the reasons for the ban and the industry's efforts to find replacement substances for the banned chemicals.
Strictly Boring: Turning Performance
Article October 1, 1995 Harvey Patterson
Strictly Boring: Turning Performance
When machinists plan a boring operation, they must rely on general turning data. Typically, this data is developed from OD turning operations, not boring operations. This article provides cutting data and recommendations specifically for boring that take into account such unique problems as boring bar deflection and chips trapped inside the bore.
Milling Inserts Shape Up
Article September 1, 1995 Ken Booker
Milling Inserts Shape Up
Changes in milling practices have placed new demands on the cutting tool. This article discusses the features toolmakers have added to their milling insert geometries to control chips and cutting forces. The article also reviews the milling process and the forces that act on the insert.
Thread Rolling on CNC Machines
Article August 1, 1995 Al McBride
Thread Rolling on CNC Machines
Thread rolling produces external threads by forming the profile instead of cutting it. This guide covers where CNC thread rolling fits, why it can outperform cutting, and what shops should watch in setup.
Driving the Tap: Turning Performance
Article August 1, 1995 Doug Moore
Driving the Tap: Turning Performance
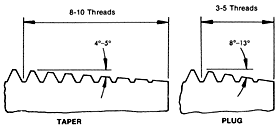
The choice of tapping driver, the component between the spindle and the tap, can affect the quality and accuracy of the threads as well as the rate of wear on the tap and the machine tool. This article discusses how features such as length compensation and self-reversing protect against damage caused by machine and tool errors.
Threads Will Roll: Drilling Performance
Article August 1, 1995 Dan Gajdosik
Threads Will Roll: Drilling Performance
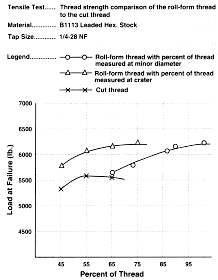
Roll-forming taps produce internal threads by displacing the metal under pressure rather than cutting it. This article explains how to perform the operation to achieve good quality threads. Formulas and charts help the user calculate the proper size hole and the size of tap to use for a desired thread.
PCBN Turns the Hard Stuff
Article June 1, 1995 Alan Carius
PCBN Turns the Hard Stuff
This article compares hard turning to grinding for finishing hardened steel parts and discusses which operation would be more appropriate for various situations. The article also looks at the machine tool, insert and cutting parameters required during hard turning.
Harder Than Anticipated: Turning Performance
Article June 1, 1995 Kevin Ackman
Harder Than Anticipated: Turning Performance
A shop supervisor and education manager recount the evolution of a job that didn't proceed exactly as planned. Because the powder-metal part was harder and its as-pressed dimensions were not as accurate as originally expected, adjustments and improvisations were needed to produce the finished parts as quickly and as cheaply as quoted.
Honing Comes Full Circle: Turning Performance
Article April 1, 1995 Guy Carmichael
Honing Comes Full Circle: Turning Performance
Honing was originally a surface finishing operation that did not remove significant amounts of material. This article discusses brush honing, a process the authors say produces results similar to what honing was originally intended to produce. Proper boring is also discussed, because, according to the authors, a properly bored hole will not require further correction through modern aggressive stone honing techniques.
Barfeeding Advances: Drilling Performance
Article April 1, 1995 Dave Poling
Barfeeding Advances: Drilling Performance
According to this article, the short-bar barfeeders that are on the market today are not plagued by the drawbacks that have become associated with barfeeding. The units load 5-foot bar stock into a lathe rather than the longer stock loaded by earlier units.

Keep exploring