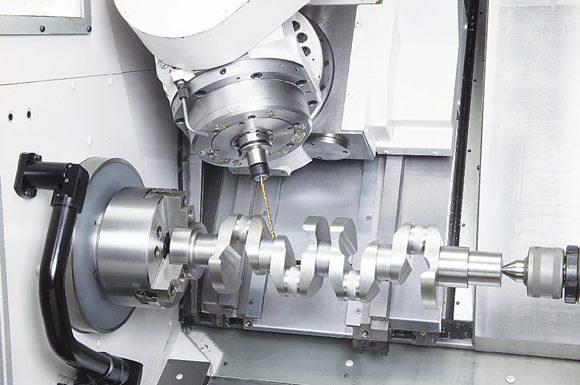
Say your machine shop just received an order for 316 stainless fuel-injector nozzles requiring angled holes to be drilled on the workpiece face. Or perhaps your best medical customer needs miniature blood-pump impellers with complex 3-D blade geometries like those on a jet-engine turbine. How are you going to make them?
When turning 2mm-dia. and smaller parts on a Swiss-style machine, it only makes sense that the radius on the tool should be equally tiny. After all, you can't cut a 0.5mm bone screw with a TNMG-431 insert—the tool's nose radius is nearly as big as the part.
Thinking about taking the leap into milling hardened steels? Why would you? After all, if your shop has been successfully grinding, jig boring and EDMing hardened materials, why change?